What Are the Top 10 Production Line Automation Solutions?

Production line automation is not a single machine or software package. It is a coordinated system that moves materials, guides work, checks quality, and shares information across a factory. A robot may load a press, while a vision camera checks a seam and sensors track temperature. When these tools work together, teams can reduce repetitive handling, improve consistency, and spot delays sooner. The gains depend on the process, though. Automation can also make a poorly designed workflow faster at producing the same problems.

Taiichi Ohno, a key architect of the Toyota Production System, is often credited with the principle, “Without standards, there can be no improvement.” That idea matters when choosing automation. Reliable results start with clear work methods, measurable targets, and practical maintenance plans—not simply buying the newest equipment. Still, standards do not solve everything. A polished diagram can hide a clumsy handoff between stations, and a small sensor issue can stop an entire line.

This overview examines ten production line automation solutions, including industrial robots, collaborative robots, conveyors, machine vision, programmable controllers, manufacturing execution systems, automated inspection, autonomous mobile robots, predictive maintenance, and digital twins. Each option serves a different purpose. Some improve throughput; others support traceability, safer material movement, or faster fault detection. The right choice depends on product mix, floor space, staffing, and existing equipment. There is no universal winner. The useful question is where automation removes a real constraint—and where human judgment should remain in the loop.
What Are the Top 10 Production Line Automation Solutions?

IFR Baseline: 4.28 Million Industrial Robots Operated Worldwide in 2023

The International Federation of Robotics (IFR) reported 4.28 million industrial robots operating worldwide in 2023, a 10% rise from 2022. Its World Robotics 2024 report also recorded 541,302 new installations that year. The installed base is the headline: automation is no longer limited to isolated robot cells. It is becoming part of everyday production infrastructure.

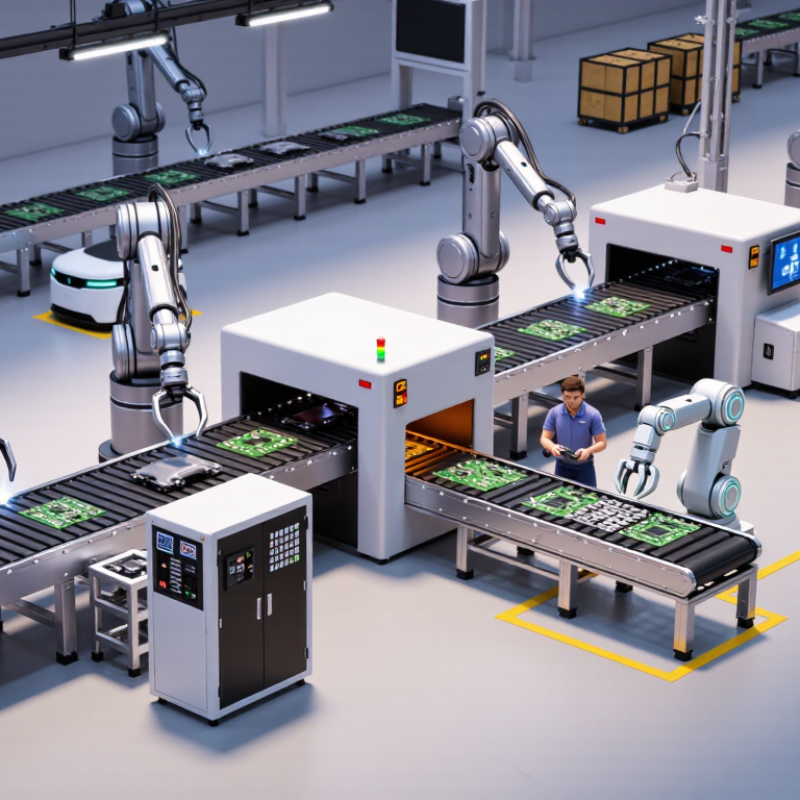
Across production lines, common solutions include machine tending, welding, assembly, pick-and-place, palletizing, packaging, dispensing, visual inspection, autonomous material movement, and production-data monitoring. A robot might lift a metal part from a machine, while a vision system checks its edge for defects. Nearby, a mobile robot can move finished trays between workstations. Small delays still matter.

IFR’s World Robotics 2023 report counted 553,052 installations in 2022, slightly more than in 2023. That comparison cautions against treating growth as a straight line. Robot counts also reveal little about utilization, integration costs, or whether workers received enough training. Scale matters. For manufacturers weighing automation options, the figures show broad adoption, not guaranteed payback. A practical assessment should examine cycle times, product variation, safety needs, and maintenance capacity before selecting a solution.

Robotic Arms and Cobots: Automating Repetitive Assembly and Handling

Robotic arms and collaborative robots, or cobots, can automate repetitive assembly and handling without requiring every station to use the same setup. An arm can place a molded part into a fixture, hold it steady, and fasten a screw at a consistent angle. Cobots are often selected for tasks near workers, such as feeding components or moving finished pieces between benches. The right choice depends on payload, reach, cycle time, and how the work area is arranged.

Start by observing the task at the actual workstation. Note where parts arrive, how they are oriented, and whether operators need to adjust them by hand. A camera may help identify part position, while a simple gripper may be enough for uniform components. Small details matter. A slippery surface or a tight cable can cause missed picks and unplanned stops. In practice, the first layout is often wrong.

Cobots are not automatically safe just because they work near people. Integrators should assess contact risks, tool edges, pinch points, and stopping distance, then configure safeguards for the specific task. Clear access for maintenance matters too. A cell that saves seconds but blocks a worker’s reach may create new delays. Pilot the setup on one station, record cycle time and stoppages, and revise it with operator feedback.

Conveyors and AGVs/AMRs: Streamlining Material Flow Across the Line

Conveyors, AGVs, and AMRs solve different material-flow problems. A belt conveyor can move cartons steadily between packing and inspection, while powered rollers let operators accumulate boxes before a busy station. AGVs generally follow defined routes; AMRs can adjust their paths around obstacles. Keep lanes clear. The International Federation of Robotics reported 113,000 professional service robots sold for transportation and logistics in 2022, 44% more than in 2021, in its World Robotics 2023 report. The figure signals growing adoption, not guaranteed savings for every factory.

Match the system to the work. Conveyors suit predictable, high-volume transfers, but a fixed line can become a bottleneck when product mix changes. AGVs can serve repeatable delivery loops, while AMRs may help when routes shift or aisles are shared. At handoff points, check turning space, floor condition, and queue length; a small jam can delay several stations. MHI and Deloitte’s 2024 Annual Industry Report found that 55% of surveyed supply-chain leaders planned to increase technology investment. That broad figure is not specific to material handling. Pilot one route, record delivery time and idle waits, then revisit the layout. The awkward part? Sensors and software cannot fix a poorly placed pickup point.

Machine Vision and AI Inspection: Detecting Defects at Production Speed

Machine vision and AI inspection help production teams find defects without slowing the line. Cameras capture each item as it passes, while trained models flag scratches, missing components, uneven seals, or incorrect labels. A clear image matters. Glare from a polished surface can hide a hairline crack, while a slight change in camera angle may trigger false alarms.

Reliable inspection starts with consistent lighting, camera placement, and product positioning. For example, a ring light can reduce shadows around a molded part, and a fixed camera distance keeps images comparable. Models should be tested with real production samples, including acceptable variations and known defects. Teams also need a process for reviewing flagged images and updating the system when materials or designs change. Small shifts can matter.

Speed is only useful when accuracy holds up across a full shift. Track missed defects, false rejects, and inspection delays, then compare those figures with manual checks. Still, no system is perfect. A model may overlook a rare flaw it has never seen, or reject a sound part because of an unusual reflection. Human review remains valuable for uncertain cases, especially during setup and after process changes. The awkward part is that maintaining this feedback loop takes time, but skipping it can quietly erode trust in the inspection results.

What Are the Top 10 Production Line Automation Solutions? - Machine Vision and AI Inspection: Detecting Defects at Production Speed

# Inspection solution Typical defects or checks How it keeps pace with production Best-fit applications Key consideration
1 2D area-scan vision Missing components, surface marks, incorrect assembly, presence or absence Captures a full image of a stationary or indexed part; exposure and processing are synchronized with the line cycle. Assembly verification, packaging, printed parts, flat surfaces Lighting, focus, and part position strongly affect image quality.
2 Line-scan vision Continuous surface defects, streaks, edge damage, print or coating variation Builds an image line by line as material moves past the camera; suitable for continuous webs and fast-moving surfaces. Paper, film, metal strip, textiles, and other continuous materials Requires stable transport and accurate synchronization with material motion.
3 3D vision and depth inspection Height or shape deviations, dents, deformation, fill level, surface profile Measures depth or surface geometry in addition to image intensity, enabling checks while parts move or are indexed. Formed components, packages, molded parts, and dimensional checks Reflective, transparent, or very dark materials may need specialized optics and setup.
4 AI visual defect classification Variable scratches, stains, cracks, cosmetic flaws, and irregular defect patterns Classifies captured images using a trained model; inference can run inline when computing capacity and cycle time are validated. Products with natural variation or defects that are difficult to describe with fixed rules Needs representative training and validation images; performance can shift when products or lighting change.
5 AI anomaly detection Unusual surface or assembly patterns not fully represented by predefined defect categories Compares production images with learned normal examples and flags deviations for inline review or rejection. Low-frequency defects and products with limited labeled defect samples Normal-product variation must be represented well to limit false alarms.
6 OCR and code verification Unreadable text, incorrect labels, missing codes, duplicate or mismatched identifiers Reads characters or machine-readable codes during the normal pass and compares results with production data. Labels, cartons, bottles, components, and traceability checkpoints Print contrast, glare, motion blur, and code quality influence reading reliability.
7 Multi-camera inspection cell Defects on multiple sides, hidden features, connector or component presence Uses several synchronized views to inspect different surfaces within one station or indexed cycle. Complex assemblies and parts that cannot be fully checked from one viewing angle Camera placement, occlusion, and coordinated lighting require careful cell design.
8 Hyperspectral or multispectral inspection Material differences, contamination, moisture variation, or defects with spectral contrast Analyzes selected wavelength bands as products pass the sensor; processing and acquisition must match line speed. Food, recycled materials, coatings, and material sorting Higher data volume and application-specific calibration can increase integration effort.
9 Vision-guided robotic rejection or sorting Detected rejects, mixed product types, orientation errors, or out-of-spec items Links inspection results to a timed air jet, diverter, or robot so actions occur at the correct product position. Packaging, picking, sorting, and automated removal of nonconforming parts Requires reliable part tracking and reject confirmation to prevent missed or incorrect ejections.
10 Closed-loop inspection and process feedback Recurring defect trends, dimensional drift, process variation, and rising reject rates Aggregates inspection results and sends approved alerts or adjustments to operators or control systems during production. Lines where inspection findings can guide process correction and quality monitoring Set safe limits and verify control logic; inspection data alone does not establish defect cause.

Line-speed capability depends on the product, field of view, image resolution, lighting, exposure time, processing hardware, and reject mechanism. Validate performance on representative production parts and operating conditions.

CNC, PLC/SCADA, MES, and Digital Twins: Connecting Machines and Operations

A connected production line depends on ten practical solutions: CNC machines, PLCs, SCADA, MES, digital twins, industrial robots, machine vision, IIoT sensors, automated guided vehicles, and predictive maintenance. CNC equipment handles repeatable cuts and drilling. PLCs control machine actions; SCADA gives operators a live view of alarms, speeds, and temperatures. MES links production orders with actual line activity.

The bridge matters. MES can send work instructions to machines, while sensor data updates a digital twin of the process. Teams can test a schedule change virtually, then compare the predicted cycle time with the real shift.

Deloitte’s 2024 Smart Manufacturing Survey found that 86% of surveyed manufacturing executives expect smart manufacturing to drive competitiveness within five years. That is an expectation, not a guaranteed result. A digital twin can also be wrong when sensor data is missing or machine settings have changed.

Tips: Start with one bottleneck, such as a CNC cell waiting for material. Check PLC and sensor data before building a twin. Keep operators involved; their notes may reveal why a line stops. Small gaps remain. Test fixes on the floor, then update the model.