7 Tips for Choosing the Best Vision Inspection Systems
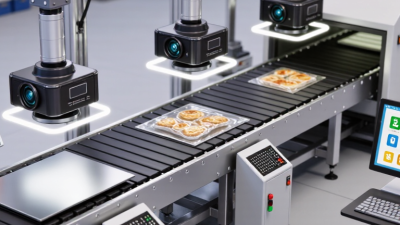
Choosing the right vision inspection systems can determine whether a production line catches defects or quietly repeats them. A camera may spot a scratched cap, missing label, or uneven seal, but reliable inspection requires more than sharp images. Lighting, optics, software, processing speed, product variation, and operator training must work together.
David Dechow, a respected machine-vision educator and industry consultant, often stresses this practical principle: “Machine vision is a systems problem, not merely a camera problem.” That idea deserves attention. A high-resolution camera cannot rescue poor lighting. Fast software cannot fix unstable product positioning. The details matter.
This guide presents seven practical tips for evaluating vision inspection systems. It considers inspection accuracy, integration, scalability, maintenance, data handling, and total ownership cost. It also examines real production conditions, including dust near a conveyor, reflective packaging, changing product colors, and limited floor space.
Specifications can look impressive.
Yet performance claims need context. A system tested on clean samples may struggle with real defects, vibration, or shifting backgrounds. I have seen teams focus heavily on resolution while overlooking reject timing and service access. That is an easy mistake.
The strongest choice usually begins with the defect, not the equipment catalogue. Define what must be detected, how quickly it must be detected, and what happens after rejection. Then compare systems against those realities. No solution is perfect, but a carefully tested system can deliver consistent quality, clearer traceability, and fewer costly surprises.
Define Inspection Goals and Product Requirements
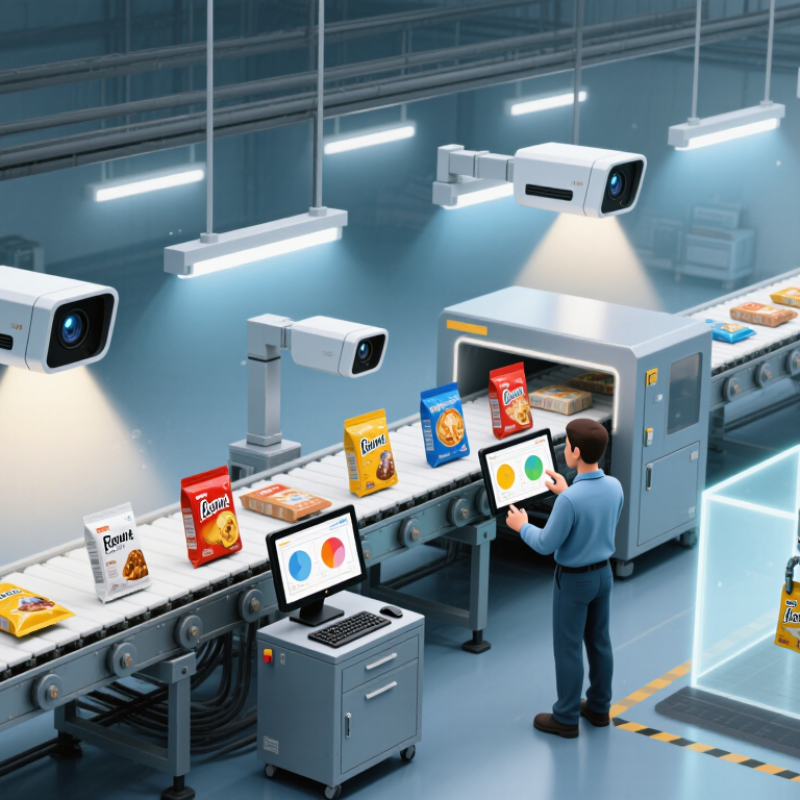
Choosing a vision inspection system starts with a precise inspection goal, not a camera catalog. Define what must be detected, measured, or verified on each product. A scratched seal, missing label, or uneven fill needs a different approach. Write the defect size, location, contrast, and acceptable tolerance. Keep it measurable. “Good appearance” is too vague. In a packaging line I supported, operators called faint wrinkles acceptable, while customers rejected them. That gap created costly rework. The requirement needed photographs and agreed samples.
Product requirements should describe real production conditions. Record dimensions, surface finish, color variation, speed, and spacing between items. Note whether products arrive warm, dusty, wet, or tilted. These details affect lighting, optics, and image-processing time. A glossy cap may look perfect under one angle and defective under another. Define the smallest defect that matters, then test it under normal and worst-case conditions. Do not rely only on clean laboratory samples. They flatter the system.
Set performance targets before demonstrations. Specify detection rate, false-reject limit, cycle time, data storage, and inspection response. Include changeover needs for different sizes. Operators may need simple adjustment screens and clear fault images. Quality teams may need searchable records by batch and time. I have seen teams overvalue headline accuracy while ignoring maintenance and training. That was a mistake. Ask for trial results using your products, including borderline examples. Leave room to revise the specification; early assumptions are often incomplete.
Compare Camera, Lighting, and Sensor Technologies
7 Tips for Choosing the Best Vision Inspection Systems
Compare Camera, Lighting, and Sensor Technologies
Tip 1: Match the camera to the defect. A global-shutter camera can capture moving parts without the skew common in rolling-shutter images. For static checks, resolution and lens quality may matter more than frame rate. MarketsandMarkets’ 2023 machine-vision report estimated the market at $12.2 billion, with projected growth to $17.2 billion by 2028. More systems are being considered, but bigger specifications do not guarantee better inspection.
Tip 2: Test lighting on the actual material. A low-angle bar light can reveal scratches on brushed metal; diffuse lighting can reduce glare on curved plastic. Try several angles and wavelengths before fixing the design. Small changes matter. Tip 3: Compare sensor types using sample parts, not catalog claims. Monochrome sensors often provide strong contrast for shape and edge checks, while color sensors help distinguish similar-looking marks. Review sensitivity, pixel size, and exposure limits; EMVA 1288 provides standardized methods for measuring camera performance.
Tip 4: Check the full image chain. Lens, lighting, sensor, and trigger timing must work together at production speed. Ask suppliers for repeatability results across clean, dusty, and changing-light conditions. I would not choose from a lab image alone. It is tempting to optimize for one perfect sample, yet real parts vary—and that is where a system can disappoint.
Evaluate Accuracy, Speed, and System Reliability
Choosing a vision inspection system means balancing accuracy, speed, and reliability on your actual production line. A published industrial anomaly-detection benchmark contains 5,354 images across 15 object and texture categories, illustrating how defect appearance varies widely. Treat that figure as a reminder, not a performance guarantee. Test with representative parts, including scratches, dents, glare, and acceptable surface variation. Measure false rejects as well as missed defects; a high accuracy score can hide costly errors.
Tip: Set a measurable accuracy target, then test it under changing light and product conditions. Check whether the system catches small defects on moving parts, not only clear defects on stationary samples. Record inspection speed at the required production rate. A system that performs well in a short demo may struggle when parts arrive close together. No threshold is perfect.
Reliability depends on more than the camera. Review uptime records, fault alerts, recovery steps, and how quickly operators can clean or recalibrate the setup. Ask for results from sustained trials on your own line, including shift changes and routine stops. ISO/IEC 25010 defines reliability as a software quality characteristic, but real production evidence matters too. One overlooked detail: a useful system should explain why it rejected a part, not merely flash a red light.
7 Tips for Choosing the Best Vision Inspection Systems - Evaluate Accuracy, Speed, and System Reliability
| Tip |
What to Evaluate |
Useful Measure or Check |
How to Verify It |
| 1. Define the inspection task |
Specify defects, acceptable variation, product presentation, and inspection coverage before comparing systems. |
Document defect types, minimum defect size, inspection area, and required decision (pass/fail, measurement, or classification). |
Create a written requirements list using representative good parts and known defect samples. |
| 2. Test accuracy on representative samples |
Check both missed defects and false rejects; overall accuracy alone can hide poor performance on rare defects. |
Measure defect-detection rate and false-reject rate separately on a labeled test set. Targets depend on defect risk and process requirements. |
Use samples not used for setup, include borderline cases, and record results by defect type. |
| 3. Match resolution to the smallest feature |
Confirm that the camera, lens, working distance, and field of view can resolve the smallest feature of interest. |
Estimate object-space pixel size as field of view divided by image pixels across that field; practical detectability also depends on contrast, optics, and lighting. |
Capture images at the intended production setup and verify that the smallest relevant feature is clearly distinguishable. |
| 4. Check speed at the required throughput |
Assess the complete cycle, including image capture, processing, communication, and reject-actuation time. |
Compare measured cycle time with the available time per part at the target line rate, including any required timing margin. |
Run a sustained trial at production speed and confirm that images and inspection decisions are not dropped. |
| 5. Evaluate lighting and environmental tolerance |
Consider glare, shadows, changing ambient light, vibration, dust, temperature, and product-surface variation. |
Review image consistency across expected operating conditions and check that enclosure and component ratings fit the installation environment. |
Test with realistic part variation and environmental conditions; assess whether controlled illumination or shielding is needed. |
| 6. Assess reliability and maintainability |
Review uptime needs, fault recovery, service access, spare parts, software support, and calibration requirements. |
Ask for documented service procedures, recovery behavior, backup and restore options, and applicable component or enclosure specifications. |
Simulate common faults and verify alarms, safe line response, restart steps, and data recovery with the operating team. |
| 7. Plan integration and ongoing validation |
Confirm compatibility with controls, production data systems, operator workflows, and future product or recipe changes. |
Define interfaces, traceability fields, change-control steps, and a schedule for checking performance with reference samples. |
Conduct an end-to-end pilot and document acceptance criteria, user training, escalation routes, and periodic review responsibilities. |
Note: Performance thresholds are application-specific. Validate them using representative parts, production conditions, and agreed acceptance criteria.
Check Software, Integration, and Ease of Use
Software should make inspection results easy to interpret, not just produce a pass-or-fail signal. Ask for a live demonstration using parts similar to yours. Can operators adjust lighting, set tolerances, and review flagged images without digging through menus? Clear records matter, too. A timestamped image linked to each result can help teams trace recurring defects and check whether a process change actually worked.
Integration deserves the same attention. Confirm how the system exchanges data with existing equipment, such as a line controller or quality database. Test the handoff under normal line speed, including what happens when a network connection drops. Small delays can create a queue of parts. And a graceful stop is better than silent data loss.
Ease of use is practical, not cosmetic. Have the people who will run the station try routine tasks, like changing a product recipe or cleaning the camera window. If only one specialist can recover from a false reject, the setup may be fragile. That said, fewer buttons do not always mean better usability; some teams need access to detailed settings. Put that trade-off on the table. A short trial can reveal awkward steps that a polished demo misses.
Assess Total Cost, Support, and Future Scalability
A vision inspection system’s purchase price is only one part of its cost. Include lighting, lenses, integration, fixtures, operator training, spare parts, and expected downtime. Ask for an itemized estimate, including recurring calibration or software fees. Then compare costs over the system’s expected service life, not just the first year. Small costs add up. Test sample products at actual line speed; a setup that works on a bench may need more tuning on the production floor.
Tip: Check support before you buy. Ask how quickly a qualified technician can respond, what remote help covers, and which parts are kept in stock. Request clear maintenance instructions and hands-on training for operators. Even careful estimates miss something, so leave room in the budget for adjustments after installation. A friendly sales conversation is not the same as dependable service.
Tip: Plan for change. Confirm that the system can handle new product sizes, faster line speeds, or additional inspection points. Ask what expanding the setup would involve: extra cameras, computing capacity, integration work, or a production pause. Review these options against your actual floor layout and data needs. Future capacity can be easy to overestimate; document assumptions and revisit them before signing.
7 Tips for Choosing the Best Vision Inspection Systems
Assess total cost, support, and future scalability before making a purchasing decision.
This 100-point planning scorecard reflects practical evaluation priorities used in industrial automation projects. Performance and integration should be assessed together with total ownership cost, service support, and the ability to scale to future production requirements.
Planning model: normalized procurement weights, not vendor-specific performance claims.